Product Overview
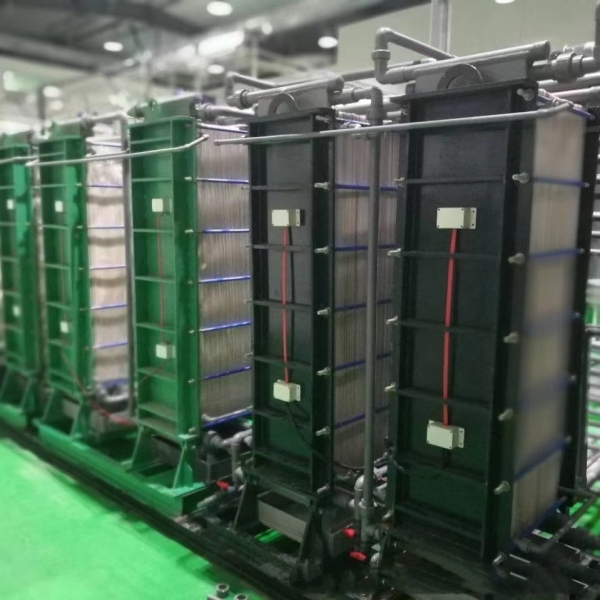
The diffusion dialysis waste sulfuric acid resource recovery system is a high-efficiency acid recovery solution that integrates microfiltration, diffusion dialysis, and nanofiltration technologies. It is specifically designed for treating by-product waste sulfuric acid generated during titanium dioxide production.
Through a multi-stage membrane separation process, the system enables efficient sulfuric acid recovery and impurity removal, significantly reducing waste acid discharge while improving resource utilization. It is suitable for large-scale continuous operation, delivering both environmental compliance and strong economic benefits.
Working Principle
The system begins with microfiltration as a pretreatment step to remove suspended solids and particulate matter from the waste sulfuric acid.
The pretreated solution then enters the diffusion dialysis unit, where sulfuric acid molecules migrate through anion exchange membranes under a concentration gradient, enabling acid recovery while separating ferrous ions.
Finally, the solution undergoes nanofiltration for polishing treatment, further removing residual ferrous ions. Through this multi-stage membrane process, high-purity sulfuric acid is obtained and can be reconcentrated as needed before being reused in the production system.
Key Features
• Integrated multi-process design: Combines microfiltration, diffusion dialysis, and nanofiltration for efficient and synergistic separation
• High recovery efficiency: Sulfuric acid recovery rate up to 88%, with recovered acid concentration ≥22%
• Excellent impurity removal: Ferrous ion rejection ≥99%, with Fe²⁺ concentration in recovered acid below 500 mg/L
• Large-scale processing capacity: Suitable for treating up to 500 tons/day of waste acid, meeting industrial continuous operation needs
• Reduced operating costs: Significantly lowers alkali consumption and solid waste generation
• Environmentally friendly: No additional pollutants generated, meeting clean production standards
Applications
• Titanium dioxide waste acid recovery: Enables resource reuse of by-product sulfuric acid and reduces discharge pressure
• High-acid wastewater treatment: Suitable for complex systems containing sulfuric acid and metal ions
• Chemical resource recycling: Recovered acid can be reconcentrated and returned to the production process
• Solid waste reduction and environmental management: Minimizes sludge and salt generation from neutralization processes
• Support for new product development: Recovered acid can be reused in new materials or process development
• Green manufacturing systems: Promotes energy saving, emission reduction, and sustainable development in the chemical industry
Performance
• Feed capacity: ~500 tons/day, sulfuric acid concentration ≥24%, ferrous sulfate <160 g/L
• Recovered acid output: ~480 tons/day, sulfuric acid concentration ≥22%, overall recovery rate ≥88%
• Ferrous ion concentration in recovered acid: <500 mg/L, corresponding to ≥99% removal efficiency
Overall Benefits
• Annual recovery of ~160,000 tons of ~22% sulfuric acid (equivalent to ~36,000 tons of 98% concentrated sulfuric acid)
• Annual savings of ~30,000 tons of neutralizing alkali, with a reduction of ~45,000 tons of solid waste
• Significant reduction in waste acid discharge and treatment burden, delivering both economic and environmental benefits